
Heat Recovery Systems Manufacturer in India
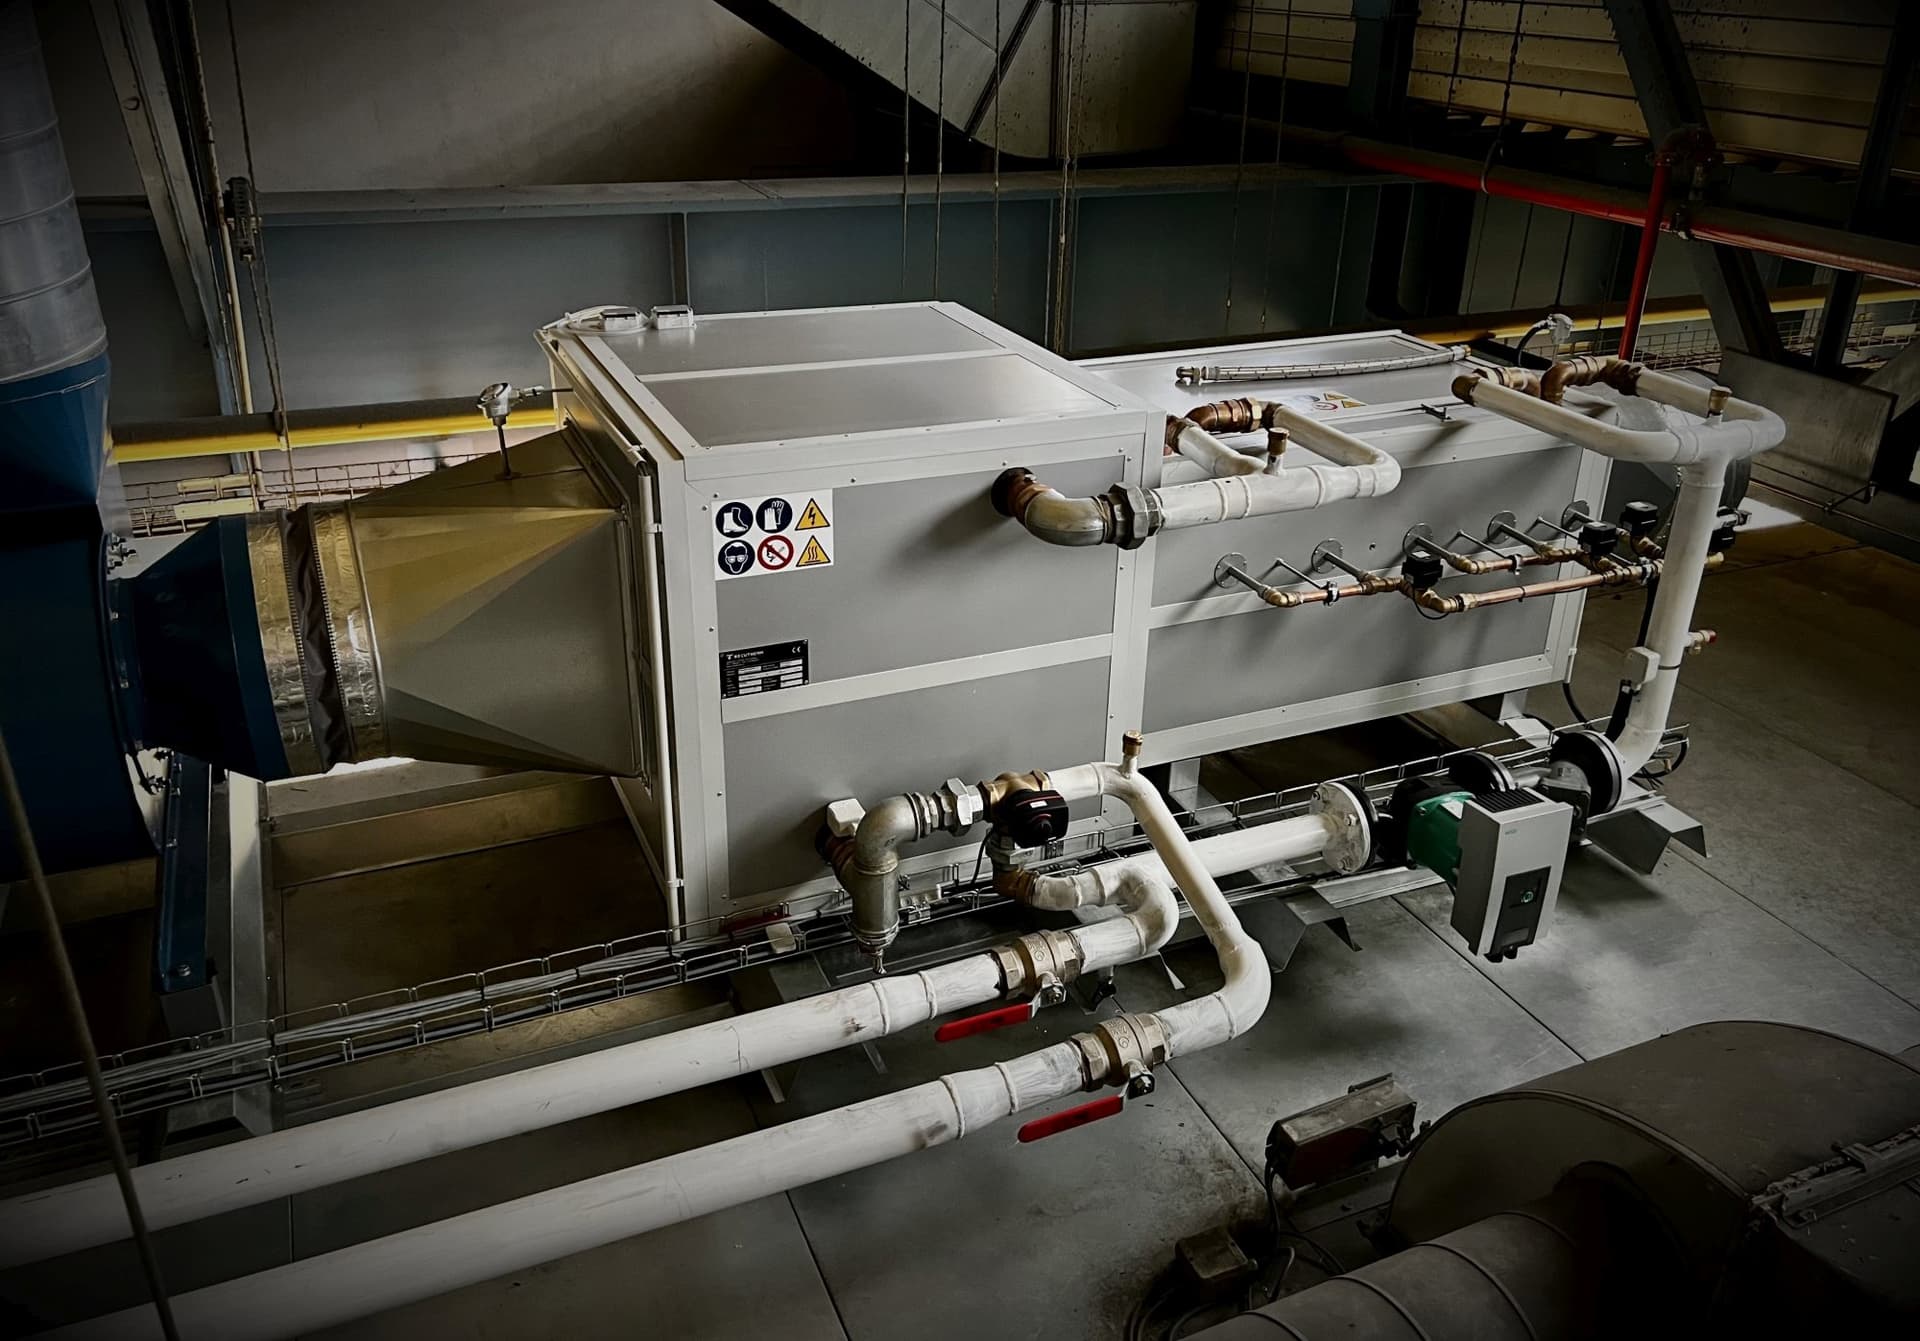
Industrial Heat Recovery Systems (WHRU) & Economizers Overview
BS Energy India manufactures high-performance Waste Heat Recovery Units (WHRU), boiler economizers, and air preheaters (APH) designed to capture waste thermal energy from stack exhaust gases and recycle it back into the plant energy cycle. Manufactured in Sholavaram, Chennai, our heat recovery units help industrial plants dramatically cut fuel consumption and carbon footprint.
In industrial boilers, thermic fluid heaters, and furnaces, flue gases frequently exit the stack at temperatures between 200°C and 450°C+, carrying away as much as 10% to 20% of the fuel's total heat value. A waste heat recovery unit installs in the flue gas path to extract this sensible heat and preheat boiler feedwater or combustion air. Every 6°C rise in boiler feedwater temperature cuts fuel consumption by approximately 1%, providing a rapid return on energy investment.
KEY TECHNICAL ADVANTAGES
Metallurgy & Heat Transfer Surface Options
Heat Recovery Equipment We Manufacture
Finned-Tube Boiler Economizers
Compact heat exchangers with spiral-finned steel tubes that preheat boiler feedwater using flue exhaust heat, boosting overall boiler efficiency.
Flue Gas Air Preheaters (APH)
Tubular heat exchangers that preheat incoming combustion air before it enters the burner, accelerating flame ignition and improving thermal efficiency.
Thermic Fluid Waste Heat Recovery Units
Recovers high-grade exhaust heat from kilns or furnaces to heat secondary thermic oil loops for process departments.
Process Water Heat Exchangers
Captures flue gas sensible heat to supply continuous hot water for process washing, CIP systems, or plant boiler makeup tanks.
Sizing Criteria & Engineering Inputs
WHRU and economizer sizing requires balancing thermal heat transfer against the maximum permissible flue gas backpressure on the existing burner and boiler. Key enquiry parameters include:
Applications of Waste Heat Recovery
Industries Served
Heat Recovery Systems is installed and operating across diverse continuous manufacturing facilities:
System Features & Bypass Dampers
- ›Flue gas ductwork modification and expansion joint installation
- ›Rigging and mounting economizer unit onto structural support stand
- ›Feedwater line tie-in: connecting feed pumps, check valves, and bypass piping
- ›Thermal performance verification: measuring stack temperature drop and fuel savings
- ›Soot removal and fin tube bundle pressure washing service
- ›Replacement finned tube spools and high-temperature gaskets
- ›Annual thermal audit and heat transfer performance recertification
WHY CHOOSE BS ENERGY INDIA FOR HEAT RECOVERY SYSTEMS
Frequently Asked Questions
How much fuel can an industrial boiler economizer save?+
A properly sized boiler economizer typically saves 5% to 10%+ in fuel consumption. As a rule of thumb, every 6°C rise in feedwater temperature reduces fuel consumption by approximately 1%.
Will installing a waste heat recovery unit create backpressure on my burner?+
We engineer economizers with optimized tube spacing and fin geometry to keep draft loss within your existing burner fan's allowable backpressure limits. Where necessary, we provide booster draft fans.
Can an economizer be retrofitted onto an existing industrial boiler?+
Yes. We frequently retrofit economizers into existing boiler houses across Chennai and India, designing custom duct transitions and feedwater bypass piping.
ABOUT BS ENERGY INDIA
BS Energy India is a manufacturer & exporter, established in 2007, operating from Sholavaram, Chennai, Tamil Nadu, India. We supply Heat Recovery Systems alongside our wider industrial heating, combustion, piping and fabrication range across India and to export markets.
Explore Related Industrial Systems
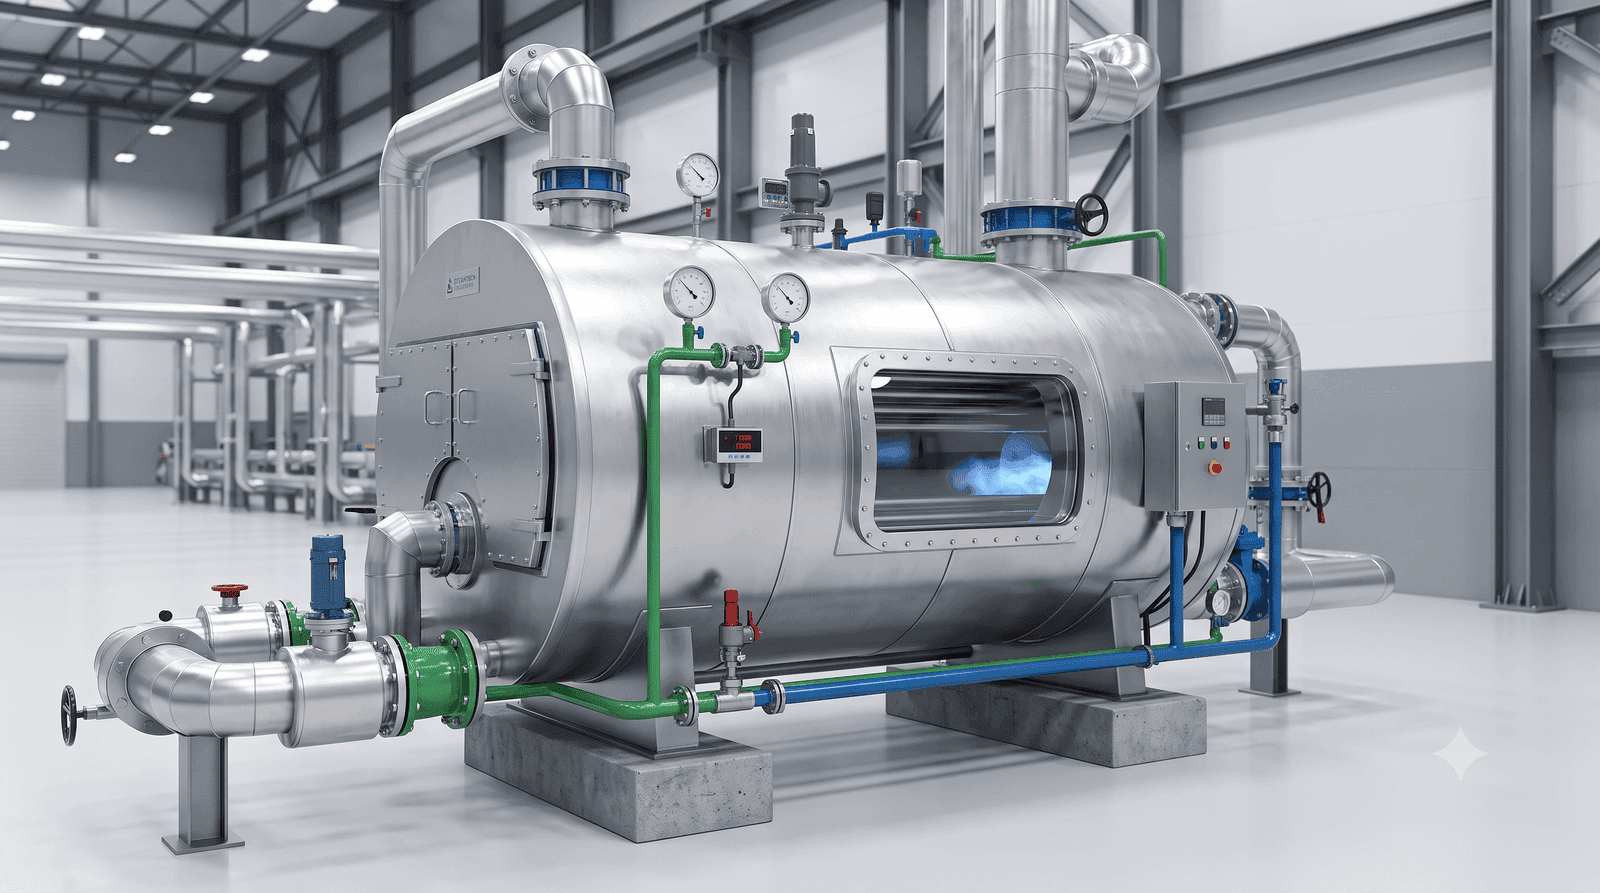
Steam Boilers
High-efficiency steam generation boilers engineered for process heating and industrial utilities.
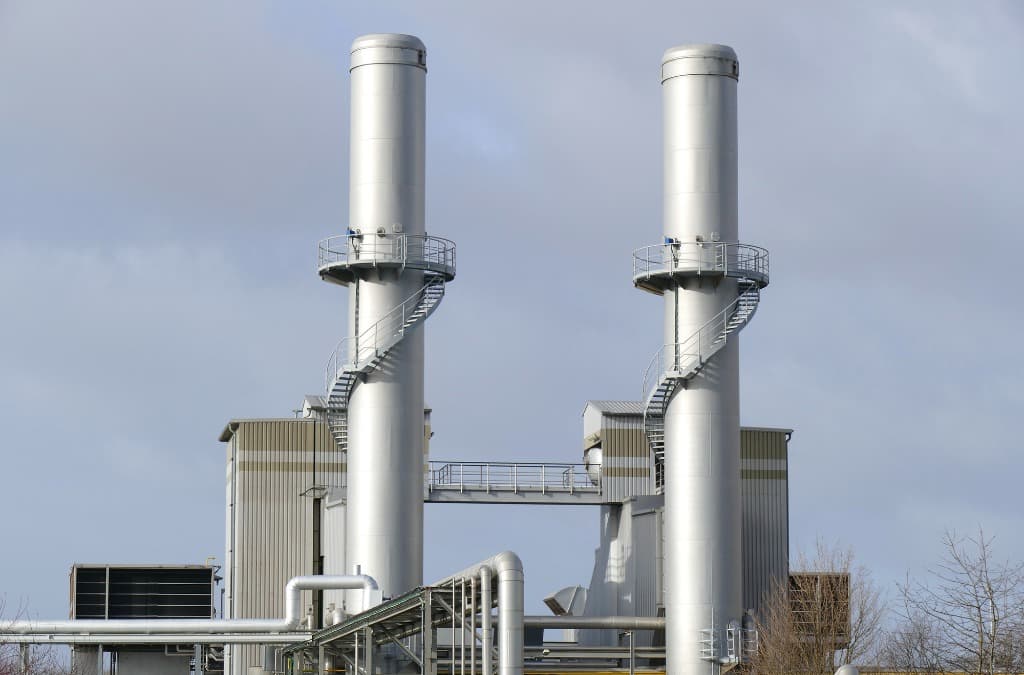
Industrial Chimneys
Engineered exhaust and stack systems designed for safe dispersion of combustion gases.
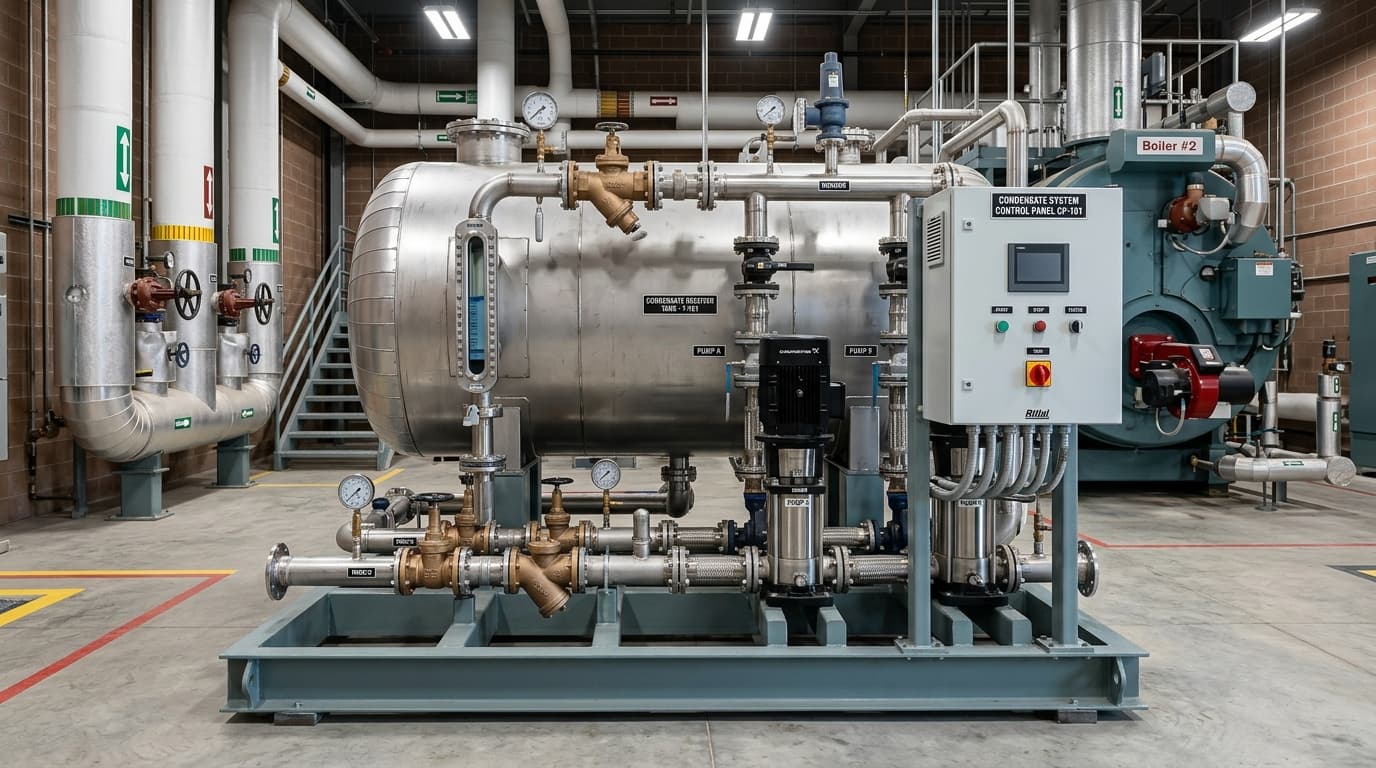
Condensate Recovery Systems
Energy-saving systems designed to return hot condensate water back to the boiler feed system.
Industrial Solar Power Systems
Turnkey rooftop and ground-mounted industrial solar PV systems and hybrid clean energy integration for manufacturing plants.