
Condensate Recovery System Manufacturer
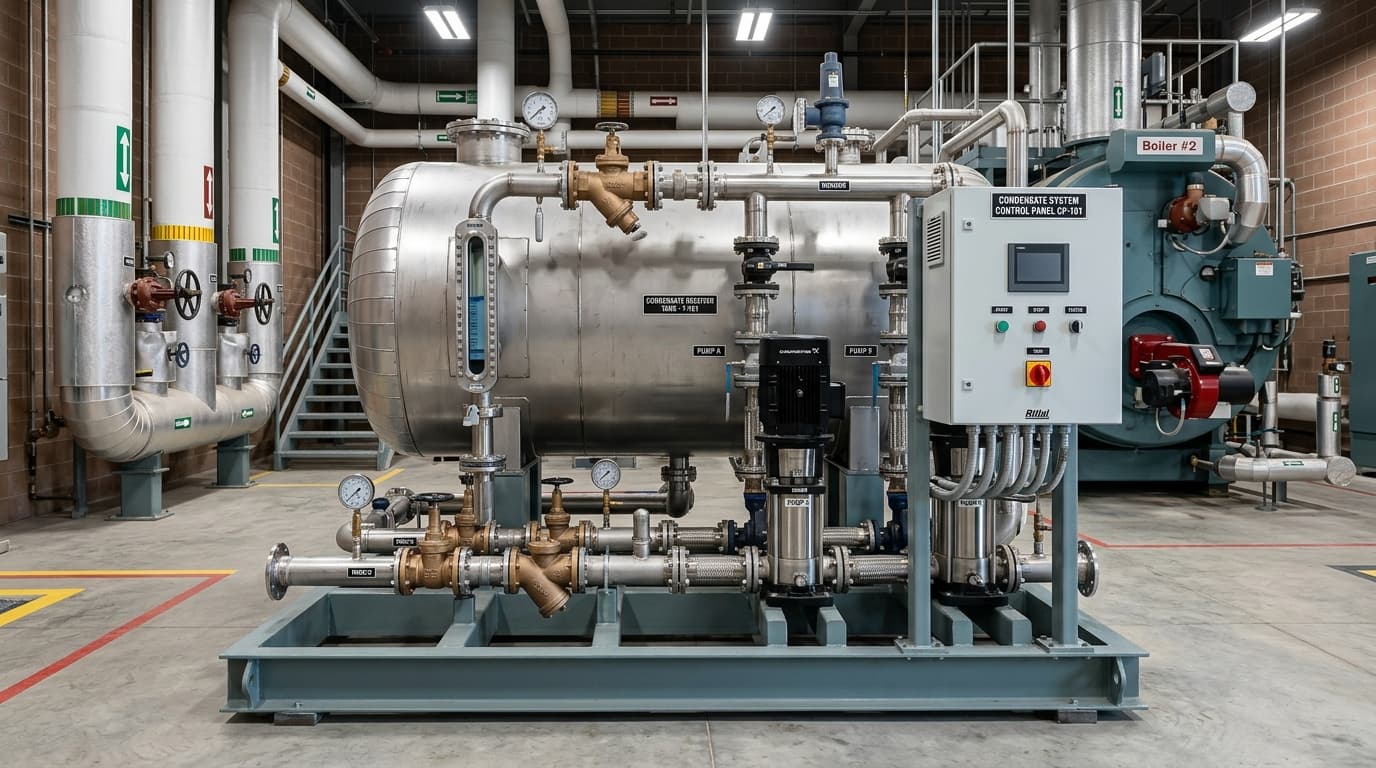
Condensate Recovery Systems — Energy Conservation Overview
BS Energy India manufactures high-efficiency Condensate Recovery Systems engineered to capture high-temperature condensate water discharged from steam traps, heat exchangers, and reboilers and pump it directly back into the boiler feedwater tank. Manufactured in Chennai, our systems recover thermal energy and cut boiler fuel and water treatment costs.
When steam releases its latent heat in process equipment, it condenses back into hot water that still retains up to 20% to 25% of the fuel energy used to generate it. Discharging condensate to the drain wastes both valuable sensible heat and expensive chemically treated demineralized water. Our condensate recovery units collect this hot condensate and return it under pressure, reducing fuel consumption by approximately 1% for every 6°C rise in boiler feedwater temperature.
KEY TECHNICAL ADVANTAGES
Materials & Skid Metallurgy
Condensate Recovery Unit Configurations
Electric Motor Pumping Skids
Heavy receiver tank coupled with duplex high-temperature multi-stage centrifugal pumps and automated level switches for continuous boiler return.
Mechanical Pressure-Powered Condensate Pumps (PPC)
Non-electric pumps operated by steam or compressed air pressure, ideal for hazardous locations, low net positive suction head (NPSH), and flood-prone pits.
Closed Pressurized Condensate Return Systems
Maintains condensate under system backpressure to prevent flash steam loss, returning water to the boiler at temperatures exceeding 100°C.
Sizing Criteria & Technical Parameters
Condensate recovery systems are sized around total condensate return volume, discharge static head, and collection line temperature. Sizing inputs include:
Applications of Condensate Recovery
Industries Served
Condensate Recovery Systems is installed and operating across diverse continuous manufacturing facilities:
System Features & Automation
- ›Positioning skid in low-elevation collection area or pit
- ›Connecting gravity condensate return manifold to receiver vessel inlet
- ›Discharge piping hookup to boiler house deaerator or feed water tank
- ›Electrical control panel wiring and automated float switch level calibration
- ›Replacement mechanical pump seals rated for high-temperature service
- ›Level switch inspection and float assembly cleaning
- ›Suction strainer screen blowdown and check valve seating inspection
WHY CHOOSE BS ENERGY INDIA FOR CONDENSATE RECOVERY SYSTEMS
Condensate Recovery Systems — Frequently Asked Questions
Why should an industrial plant invest in a condensate recovery system?
Condensate retains valuable sensible heat (up to 20%+ of boiler energy) and is pure distilled water. Returning it to the boiler feed tank cuts fuel consumption (1% saved per 6°C rise in feedwater temperature), eliminates water treatment chemical costs, and reduces water bills.
What is the difference between an electric condensate pump and a mechanical pressure-powered pump?
Electric pump skids use high-temperature motor-driven pumps for continuous high-volume return. Mechanical pressure-powered pumps use steam or compressed air pressure to pump condensate without electricity, making them ideal for hazardous explosive zones or zero-NPSH low pits.
Does BS Energy India supply both the receiver tank and the pumping skid?
Yes. Our condensate recovery units are pre-assembled on structural steel skids with the receiver tank, duplex pumps, valves, piping, level controls, and electrical panel ready for pipe hookup.
ABOUT BS ENERGY INDIA
BS Energy India is a manufacturer & exporter, established in 2007, operating from Sholavaram, Chennai, Tamil Nadu, India. We supply Condensate Recovery Systems alongside our wider industrial heating, combustion, piping and fabrication range across India and to export markets.
Explore Related Industrial Systems
Steam Boilers
High-efficiency steam generation boilers engineered for process heating and industrial utilities.
Heat Recovery Systems
Energy-saving waste heat recovery units designed to capture thermal energy from exhaust gases.
Pressure Reducing Systems (PRS)
Precision steam and gas pressure reduction stations for safe, steady line distribution.