
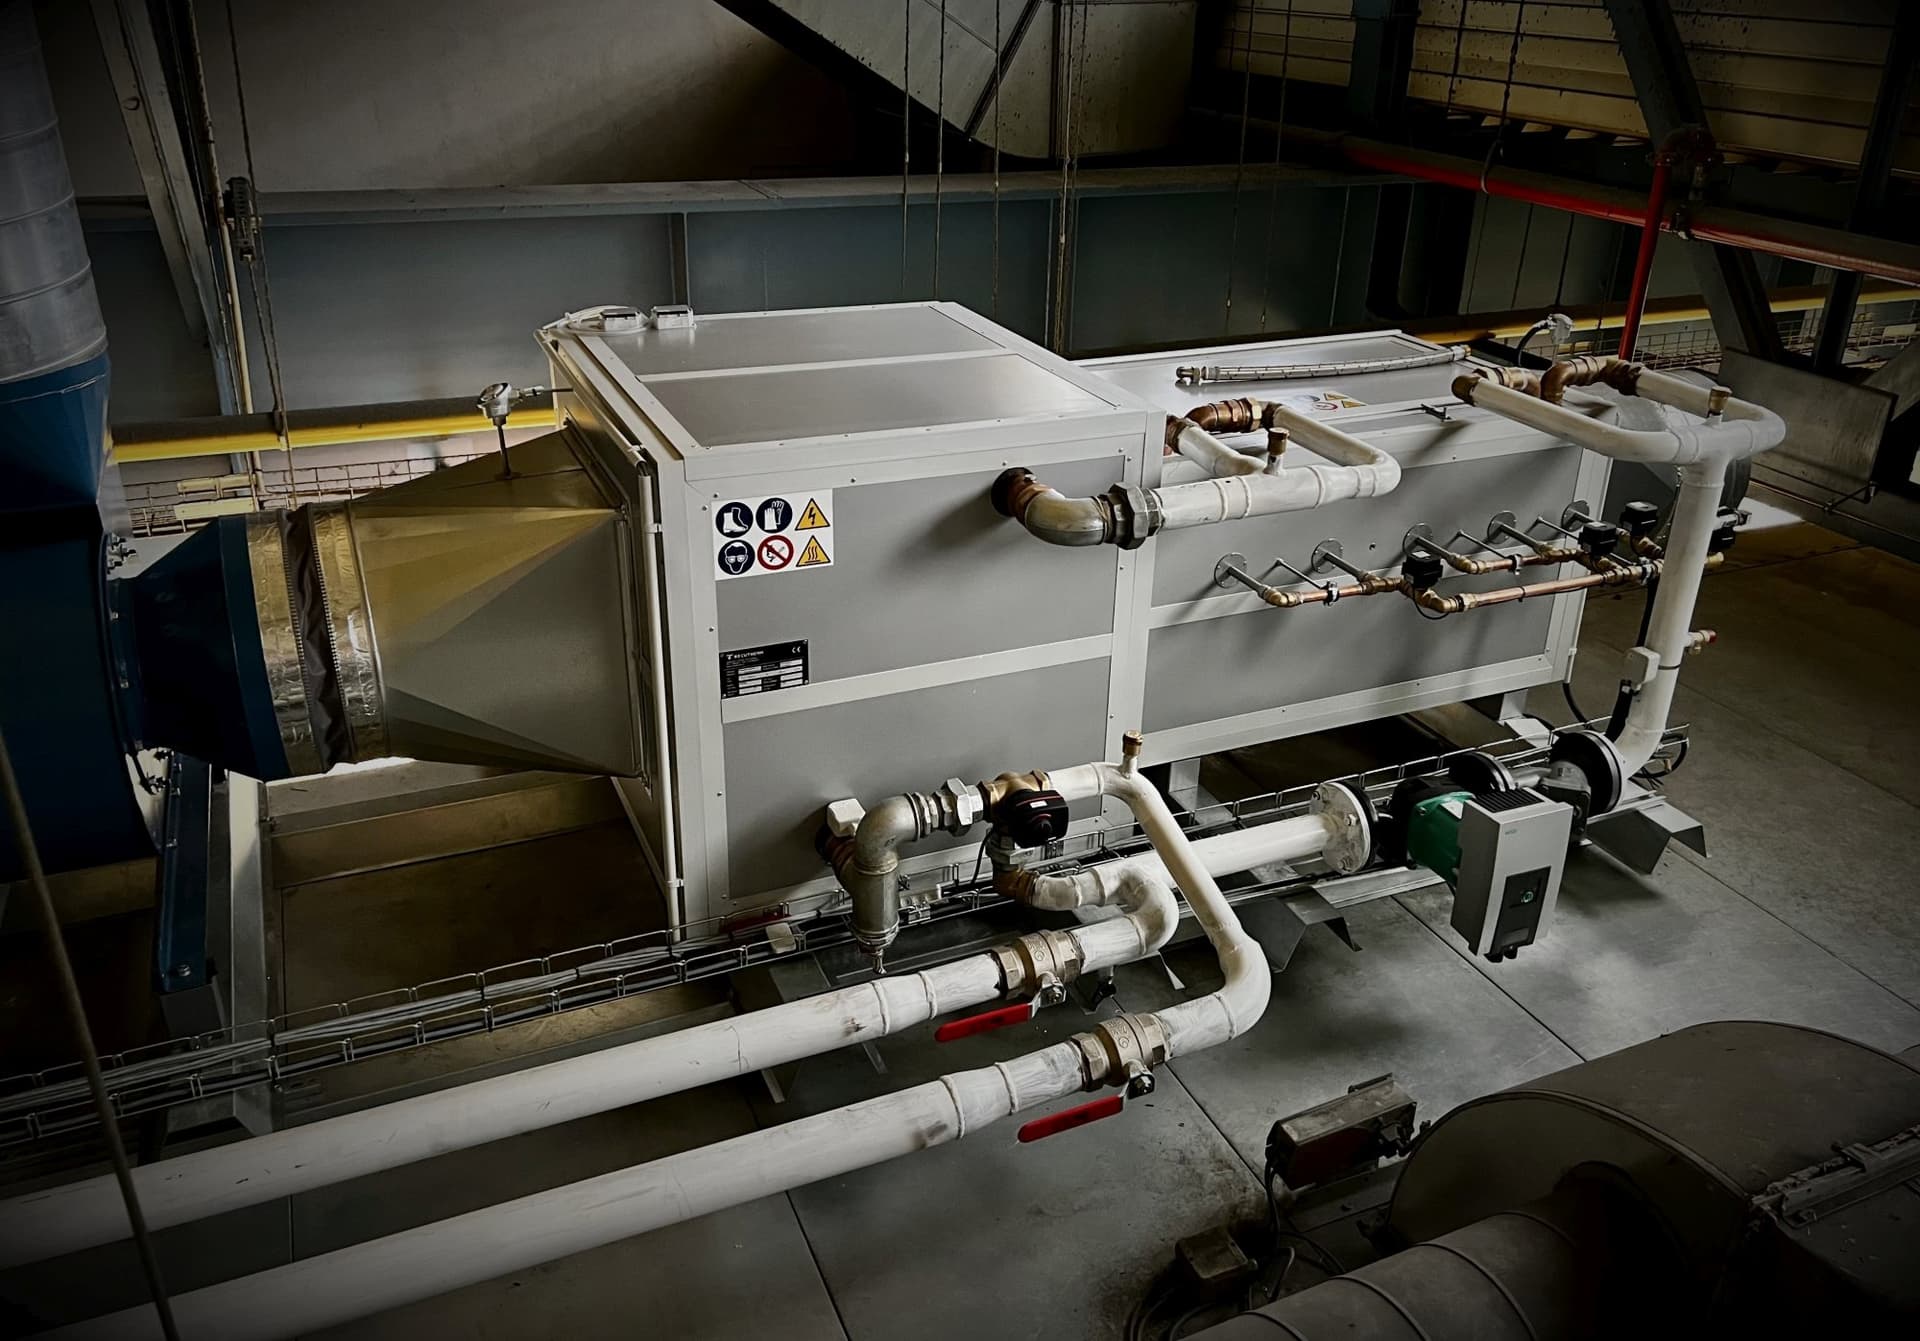
1. The Unrecovered Energy Escaping Your Boiler Chimney
In standard industrial boilers operating without heat recovery, exhaust flue gases exit through the chimney stack at temperatures between 200°C and 260°C. For heavy furnace oil or gas-fired installations, this represents an immediate loss of 8% to 15% of the fuel's chemical energy straight into the atmosphere.
2. How a Boiler Economizer Recovers Sensible Heat
A boiler economizer is a heat exchanger installed in the exhaust flue gas duct directly between the boiler outlet and the chimney stack. Boiler feedwater from the feed pump passes through finned steel tubes on its way into the boiler drum, while hot exhaust gases pass across the outside of the tubes.
3. The Rule of Thumb: 6°C Rise = 1% Fuel Saving
In combustion engineering, a proven rule of thumb governs economizer design:
For every 6°C increase in boiler feedwater temperature achieved through waste heat recovery, overall boiler fuel consumption decreases by approximately 1%. Simultaneously, every 20°C decrease in stack flue gas temperature boosts overall boiler thermal efficiency by 1%.
In a typical 5-ton-per-hour boiler operating at 10.5 kg/cm², an economizer raising feedwater temperature from 30°C to 80°C (a 50°C rise) delivers over 8% in continuous fuel savings, returning the entire capital investment within 6 to 12 months.
4. Engineering Design Factors: Avoiding Cold-End Acid Corrosion
While recovering maximum heat is desirable, the exhaust flue gas must not be cooled below its acid dewpoint. If flue gases contain sulfur (common in furnace oil and diesel), cooling below 130°C–140°C causes sulfur dioxide and trioxide to condense into sulfuric acid, causing rapid metal wastage. BS Energy India calculates exact minimum wall temperatures and incorporates modulating bypass dampers to protect equipment during startup.
Learn more about our custom manufactured Heat Recovery Systems and request an engineering site audit.
Heat Recovery Systems
Energy-saving waste heat recovery units designed to capture thermal energy from exhaust gases. Manufactured, supplied, and commissioned by BS Energy India from Chennai.
BS Energy India is a premier industrial heating, combustion, and process piping manufacturer operating since 2007 in Sholavaram, Chennai, Tamil Nadu, India. Our technical guides are authored by practicing mechanical and combustion engineers to assist industrial plant managers, utility engineers, and procurement teams.